CNC Machining Surface Roughness: How to Specify Ra for Functional Parts
A clear Ra requirement helps suppliers quote accurately, select the right toolpath, and inspect the surfaces that matter for fit, sealing, sliding, and appearance.
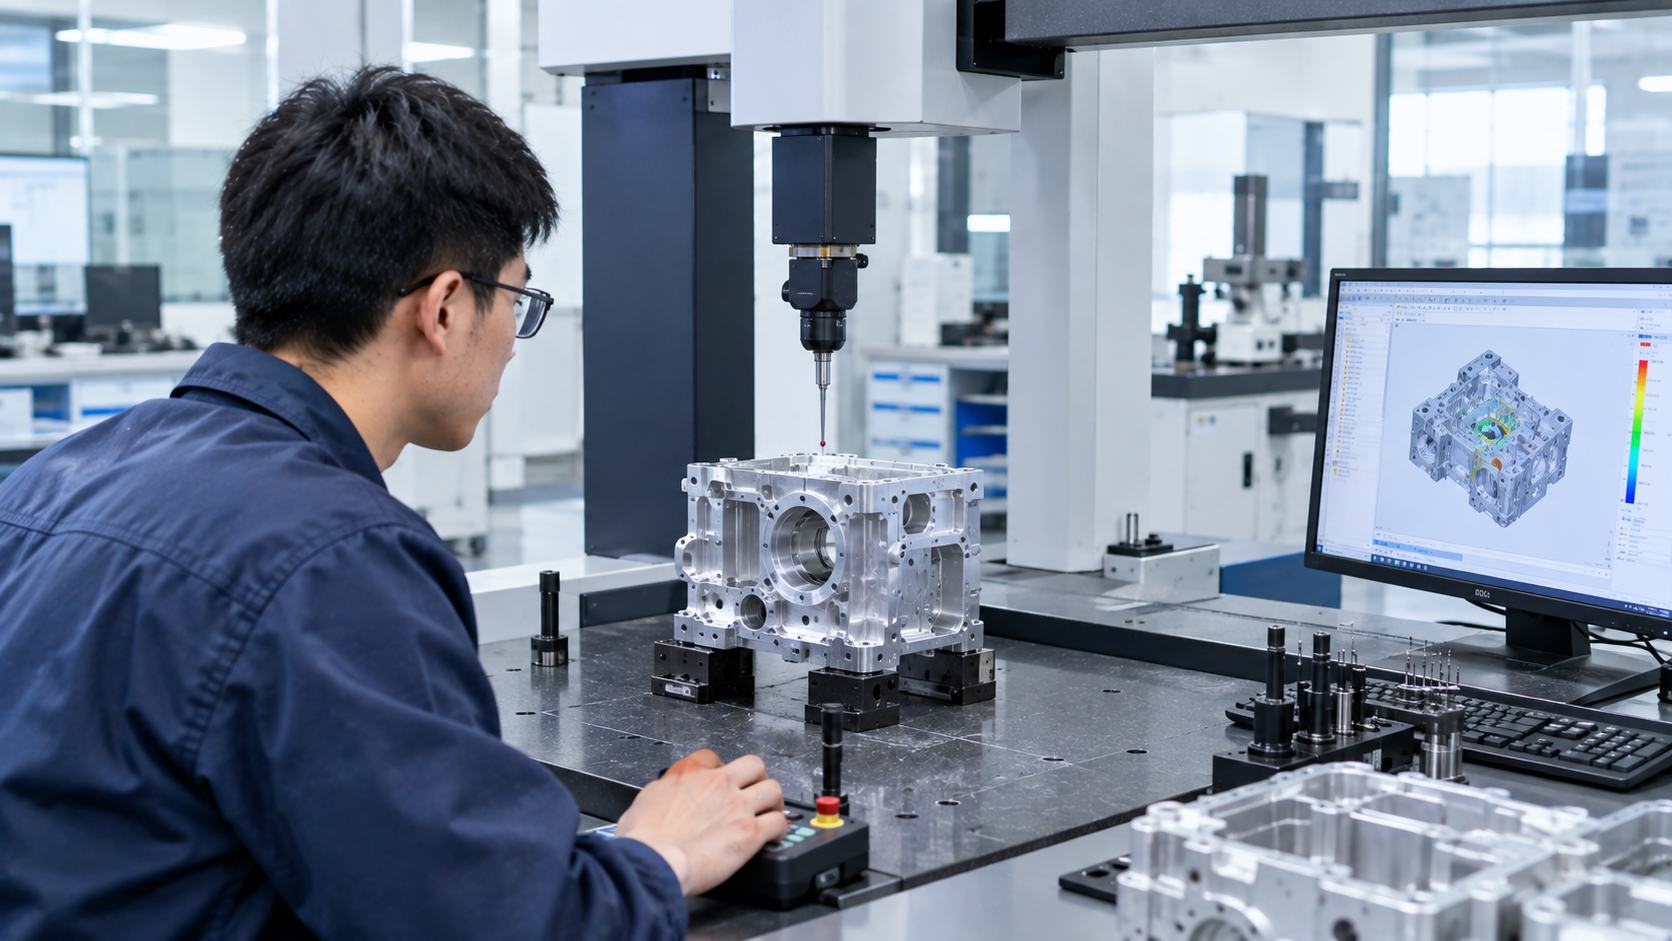
Surface roughness is often treated as a finishing note, but it can change how a CNC machined part seals, slides, mates, reflects light, or survives wear. The most useful specification is not “smooth finish everywhere”; it is a measured Ra requirement assigned to the surfaces that have a real function.
Function
Define whether the surface seals, slides, locates, mates, or is cosmetic.
Process
Choose toolpaths, cutters, feeds, speeds, deburring, and finishing around the target Ra.
Proof
Identify the datum and inspection method so the result can be verified consistently.
What Ra means in a CNC machining RFQ
Ra is the arithmetic average roughness measured over a defined sampling length. It is normally stated in micrometres, for example Ra 3.2 µm or Ra 1.6 µm. A lower number indicates a smoother surface, but it does not automatically guarantee better part performance.
| Typical requirement | Practical use | RFQ note |
|---|---|---|
| Ra 3.2 µm | General milled or turned surfaces | Good baseline for many non-sealing functional faces. |
| Ra 1.6 µm | Better mating and sliding surfaces | May require a controlled finishing pass and inspection. |
| Ra 0.8 µm or lower | Sealing, precision sliding, or high-appearance areas | Confirm process capability, measurement method, and cost before quoting. |
How to select surface roughness by function
Sealing faces and gasket lands
Sealing surfaces need a controlled finish and stable flatness. Specify the roughness on the actual sealing land, not on every face of the component, and include the gasket or seal type when requesting a quote.
Sliding and bearing interfaces
Sliding surfaces may need a smoother finish, but the material pair, lubrication, clearance, hardness, and direction of tool marks also matter. An Ra value alone is not a complete tribology requirement.
Cosmetic aluminum housings
For visible enclosures, machining marks may be intentionally blended before anodizing or bead blasting. State whether the requirement applies before or after finishing and define the acceptable visual direction.
What can change CNC surface roughness?
- Tool diameter, tool nose radius, cutter runout, and tool wear.
- Feed per tooth, spindle speed, step-over, axial depth, and toolpath direction.
- Material hardness, temper, work hardening, and machine rigidity.
- Coolant strategy, chip evacuation, burr control, and post-machining handling.
- Secondary operations such as anodizing, plating, polishing, or bead blasting.
Inspection and acceptance criteria
Agree on where the reading is taken, whether the part is measured before or after surface treatment, and which instrument or comparator is used. A supplier should also identify whether the reported result is a single reading, an average, or a range across multiple locations.
Related CNC machining resources
See our precision CNC machining capability for process scope and quality controls. For enclosure projects, review our CNC machined aluminum enclosure guide and include the required finish in your RFQ.
FAQ
Is a lower Ra always better?
No. A lower Ra can increase machining time and cost, and the correct requirement depends on the function of the surface.
Can anodizing change surface roughness?
Yes. Preparation and anodizing can change the appearance and measured result. State whether the requirement applies before or after treatment.
What should I send for a surface finish quote?
Send the CAD file, 2D drawing, material and temper, target quantities, finish schedule, and clearly marked functional or cosmetic surfaces.
Need a CNC finish review?
Send your drawing and we can review Ra, tolerances, material, and post-processing before quotation.